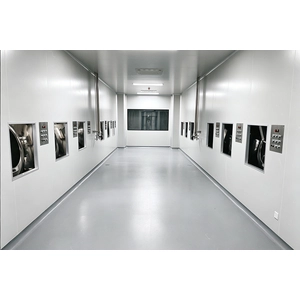
For nearly three decades, one established manufacturer has been quietly shaping the standards of suppository production, earning the trust of pharmaceutical companies, hospital pharmacies, overseas distributors, and processors across the chemical, food, and agricultural sectors. As a director unit of the China Pharmaceutical Equipment Industry Association, the company has delivered solutions to more than a thousand pharmaceutical enterprises worldwide. Its reputation rests on engineering depth, regulatory awareness, and a commitment to smart, seamless production.
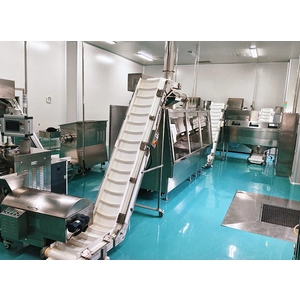
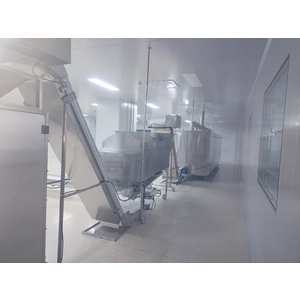
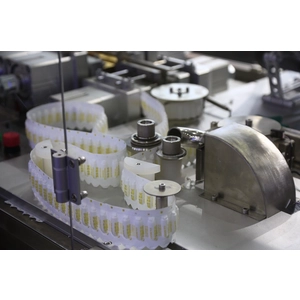
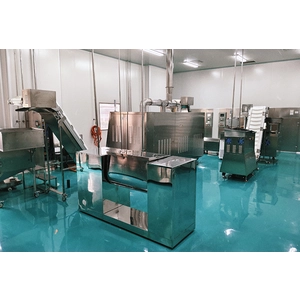
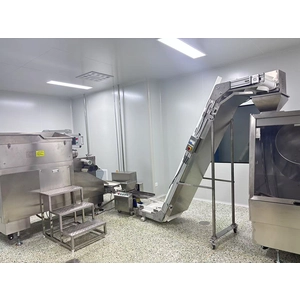
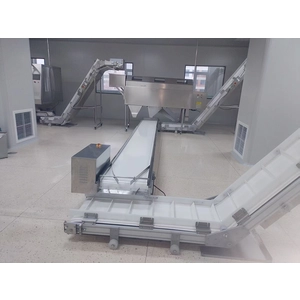
In an era where production capacity directly influences market responsiveness, the high speed suppository production line offers pharmaceutical manufacturers a decisive advantage. These integrated systems synchronise filling, cooling, sealing, and cutting into a continuous flow, with precise temperature control and accurate dosing to preserve formulation integrity. Servo-driven indexing and real-time monitoring minimise rejects while maximising throughput. For large-scale drug plants and contract manufacturers, the combination of velocity and consistency ensures that quality is never compromised by speed.
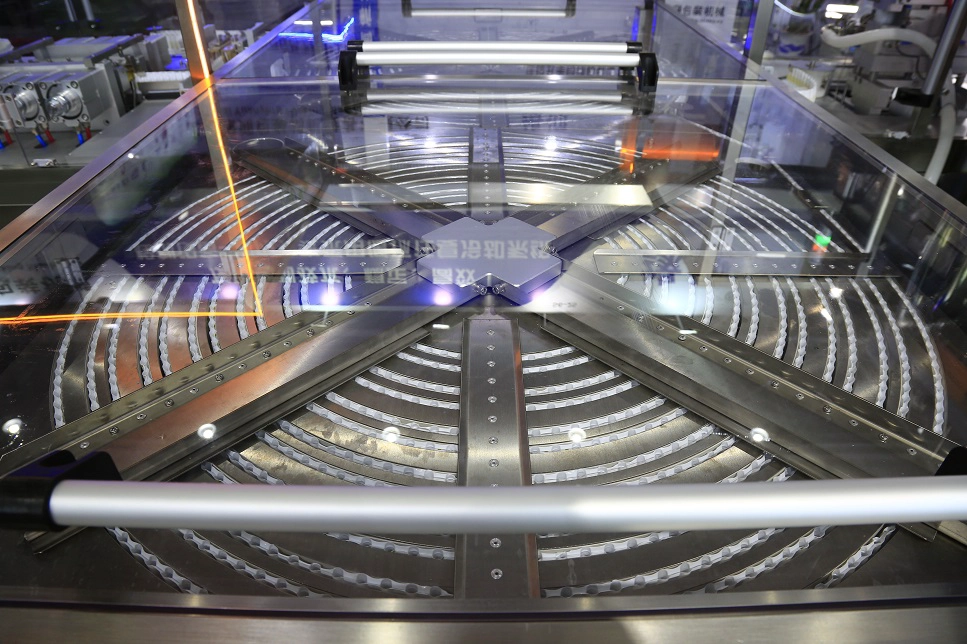
Recognising that many clients prefer a single point of accountability from design through commissioning, the company operates as a turnkey suppository production line company. Its engineers work closely with clients to assess facility layout, utility requirements, and product specifications, then deliver a complete solution encompassing equipment, installation guidance, validation support, and operator training. This integrated approach reduces coordination burden and accelerates project timelines. Hospital pharmacies and overseas dealers alike benefit from a single, experienced partner managing the entire production setup.
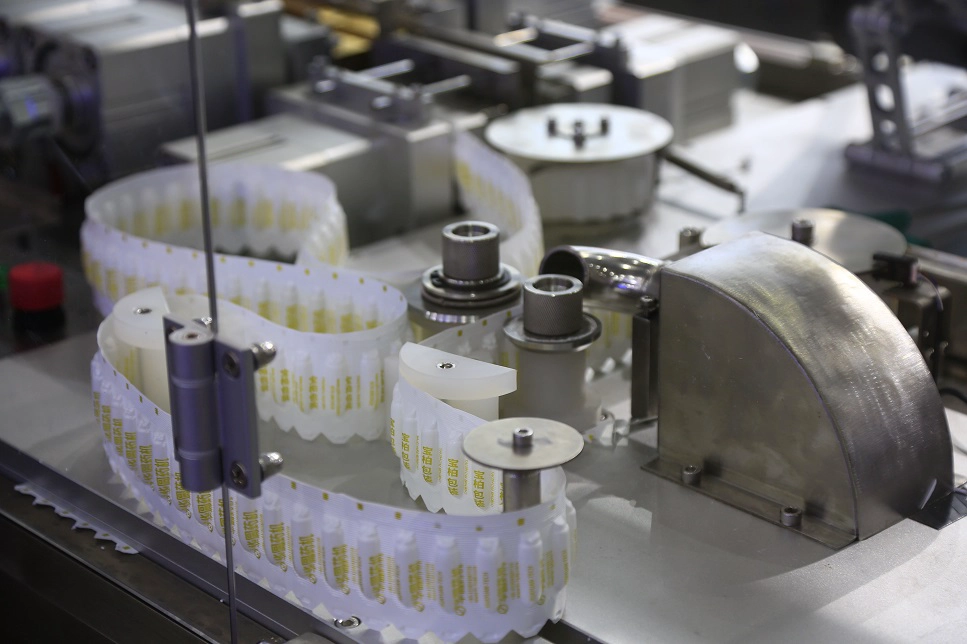
Behind every system lies a manufacturing ecosystem built on vertical integration and rigorous quality control. As an automatic suppository equipment factory china, the company oversees every stage of production, from metallurgical analysis and precision machining to final assembly and factory acceptance testing. This in-house capability guarantees complete build records, validation documentation, and consistent tolerances for regulated drug production. OEM services, private labelling, and tailored control interfaces are also available for international partners.
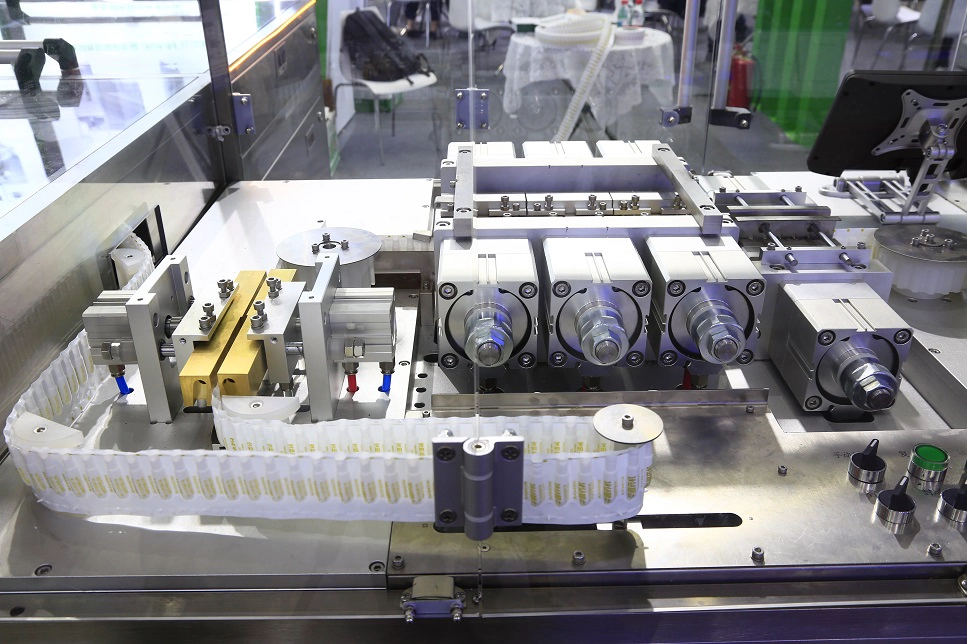
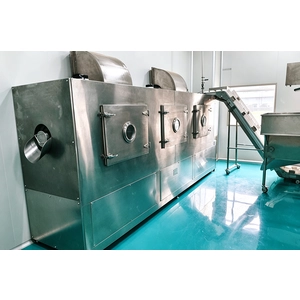
Beyond suppository lines, the portfolio includes herbal pill making machines, continuous dryers, medical sterilization units, and chemical ball formers. Each product shares the same robust construction and intelligent control architecture, reflecting a holistic approach to solid dosage manufacturing. The extensive installed base and active role in industry standards continue to drive refinements that benefit clients across multiple sectors.
Looking ahead, the manufacturer remains committed to advancing smart monitoring, predictive maintenance, and energy-efficient drive systems. Whether serving a clinical pharmacy, a high-volume drug producer, or an international distributor, it provides the engineering depth and manufacturing integrity that define enduring excellence. For global partners, choosing this heritage brand means investing in reliability that spans generations of production.

 +8613809387113