For nearly three decades, one established manufacturer has been a trusted cornerstone in pharmaceutical equipment, serving drug producers, hospital pharmacies, overseas distributors, and processors across the food, chemical, and agricultural sectors. As a director unit of the China Pharmaceutical Equipment Industry Association, the company has delivered solutions to more than a thousand pharmaceutical enterprises worldwide. Its enduring reputation is built on engineering depth, regulatory awareness, and a relentless commitment to smart, seamless production.
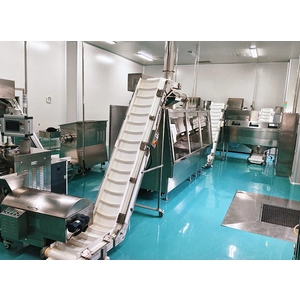
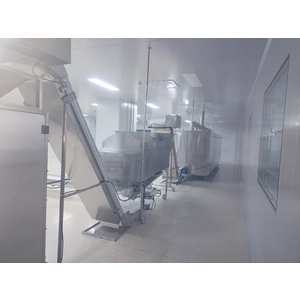
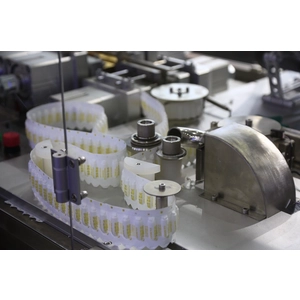
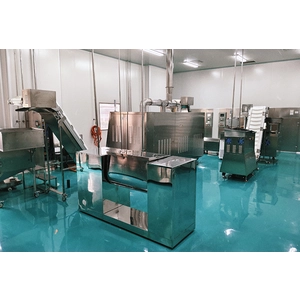
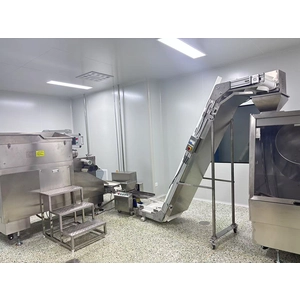
Large-scale drug manufacturing requires systems that deliver uncompromising reliability and continuous output. The automatic suppository production line B2B platform is engineered precisely for this environment, offering pharmaceutical enterprises and contract manufacturers a robust solution for high-volume operations. Featuring advanced temperature control, precise filling mechanisms, and automated sealing, these lines ensure consistent product quality across every batch. By integrating intelligent control architectures, the manufacturer provides B2B clients with seamless scalability and significantly reduced downtime.
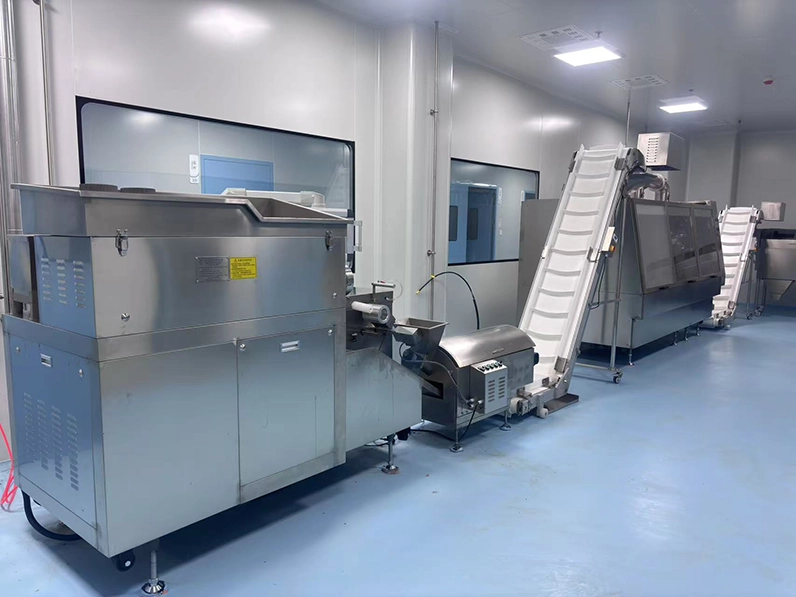
In today’s competitive market, product identity and brand recognition are just as important as operational efficiency. Recognizing this, the company offers a suppository production line custom logo service, allowing pharmaceutical brands and international distributors to integrate their own corporate identity directly into the machinery. This bespoke approach includes customized HMI interfaces, branded exterior panels, and tailored documentation packages. Such personalized engineering empowers partners to present fully branded, turnkey solutions to their own clientele, reinforcing market presence.
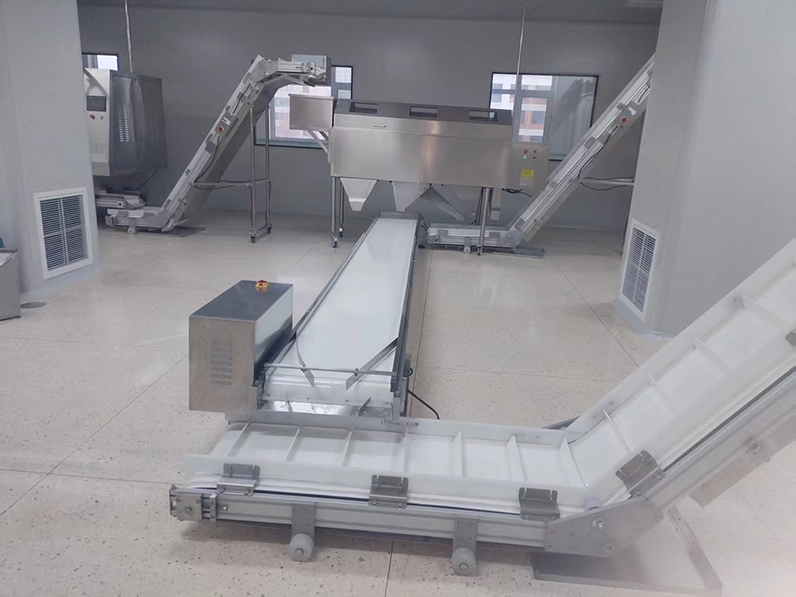
Accessibility to advanced technology is crucial for emerging enterprises and hospital pharmacies looking to upgrade their production capabilities without excessive initial expenditure. The availability of a low price automatic suppository line provides a highly efficient entry point into automated manufacturing. By standardizing non-critical components and optimizing production workflows, the manufacturer delivers reliable, GMP-compliant equipment at an accessible threshold. This cost-effective approach ensures that smaller-scale producers can still benefit from the brand’s hallmark precision and durability.
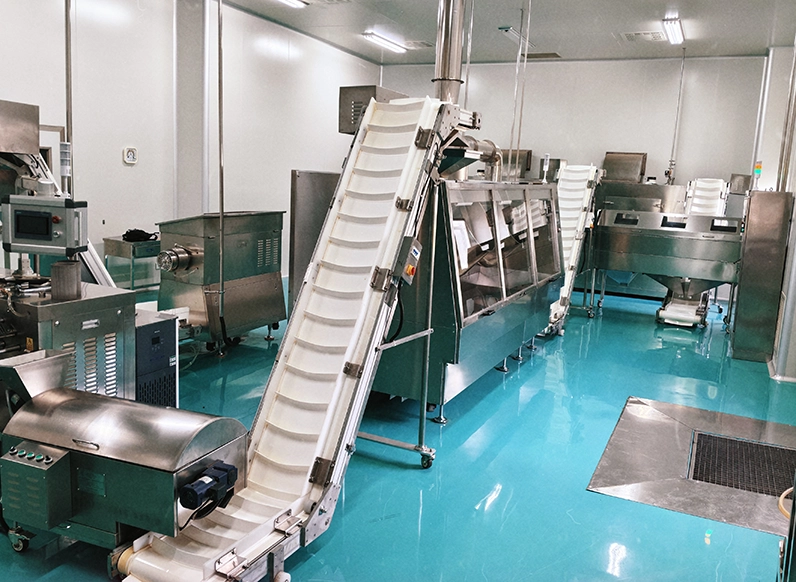
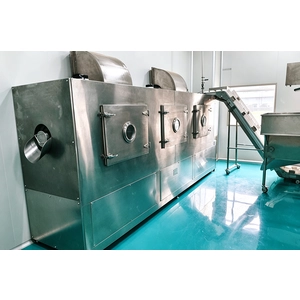
Beyond suppository equipment, the company’s comprehensive portfolio spans herbal pill making machines, continuous dryers, medical sterilization units, and chemical ball formers. Each product shares the same robust construction philosophy, designed to meet the demanding standards of multiple industries. The extensive installed base and active participation in industry standards continue to drive refinements that benefit clients globally.
Looking ahead, the manufacturer remains committed to advancing smart monitoring, predictive maintenance, and energy-efficient drive systems. Whether equipping a high-volume B2B facility, designing a custom-branded line, or providing accessible automation for growing businesses, the company provides the engineering depth and manufacturing integrity that define enduring excellence. For global partners, choosing this heritage brand means investing in reliability that spans generations of production.

 +8613809387113