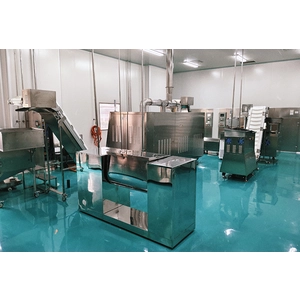
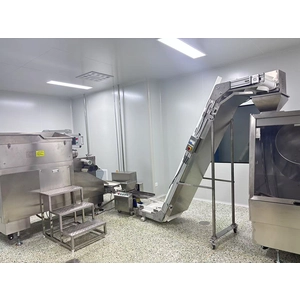
For nearly three decades, one established equipment manufacturer has been a cornerstone of pharmaceutical production, serving a diverse clientele that includes drug manufacturers, hospital pharmacies, overseas equipment dealers, and processors in the chemical, food, and agricultural sectors. As a director unit of the China Pharmaceutical Equipment Industry Association, the company has delivered solutions to more than a thousand pharmaceutical enterprises worldwide. Its enduring reputation is built on engineering depth, regulatory awareness, and a commitment to smart, seamless production.
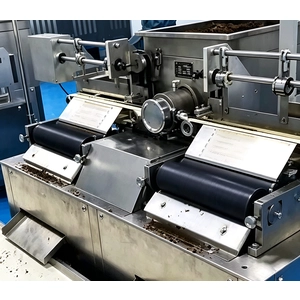
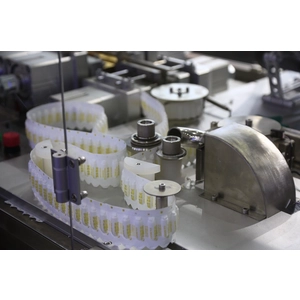
The quality of a suppository begins with the integrity of its shell. The pvc pe suppository shell machine is engineered to handle the precise thermal and rheological properties of polymer materials, ensuring consistent melting, molding, and cooling. By maintaining strict control over temperature zones and cycle times, the equipment produces uniform shell thickness and flawless surface finishes. Pharmaceutical manufacturers rely on this precision to guarantee proper drug release profiles and long-term stability, even for highly sensitive active ingredients.
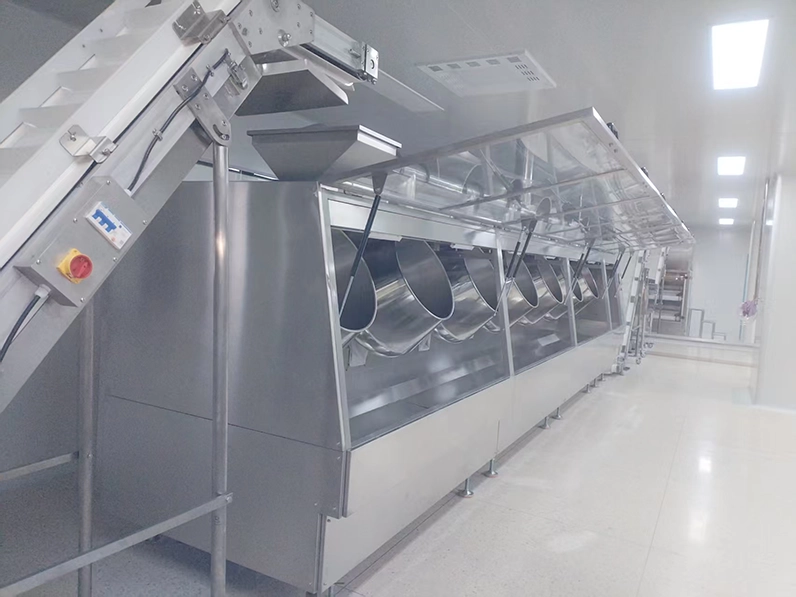
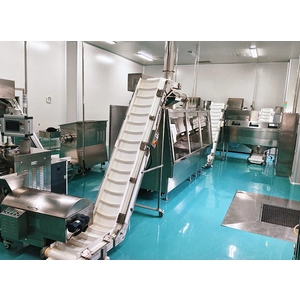
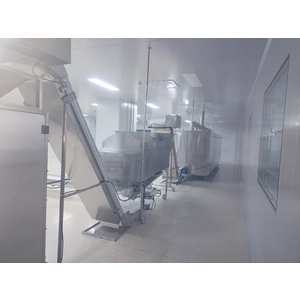
Automation is essential for scaling production while maintaining strict hygiene standards. The automatic suppository shell forming machine integrates intelligent PLC controls, high-efficiency cooling systems, and automated demolding mechanisms into a continuous workflow. This reduces manual intervention, minimizes waste, and ensures that every shell meets rigorous GMP compliance. Whether operating a high-volume pharmaceutical plant or a specialized compounding facility, manufacturers benefit from rapid cycle times and repeatable output quality.
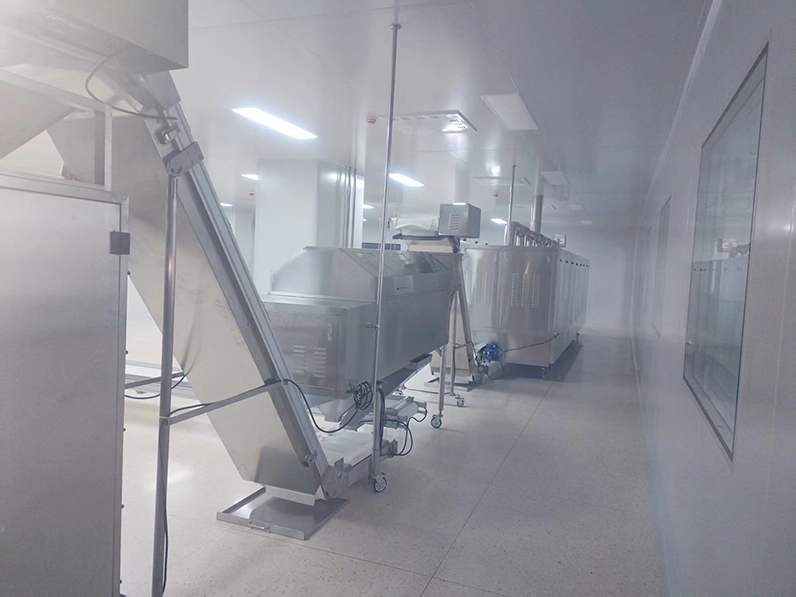
Transparency and direct communication are central to the company’s customer philosophy. By providing the suppository shell machine factory direct model, the manufacturer eliminates unnecessary intermediaries and connects end-users directly with its engineering team. This direct channel enables rapid customization of mold geometries, tailored control interfaces, and immediate access to technical support. Moreover, factory-direct procurement ensures complete build records and validation documentation, simplifying regulatory submissions for global partners.
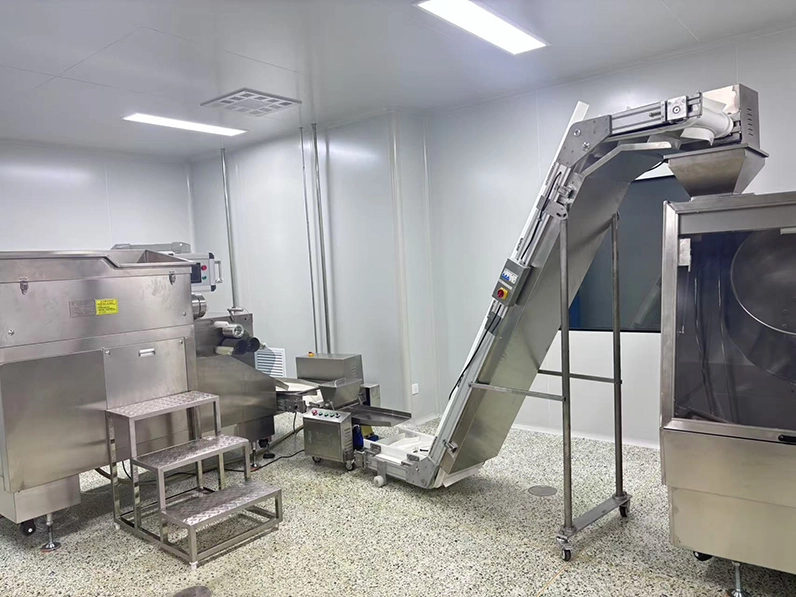
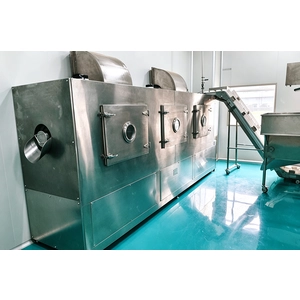
Beyond shell-forming technology, the company’s comprehensive portfolio includes fully automatic suppository filling and sealing lines, herbal pill making machines, continuous dryers, and medical sterilization units. Each product shares the same robust construction philosophy, designed to meet the demanding standards of the pharmaceutical, food, and chemical industries. The extensive installed base and decades of field feedback continue to drive refinements that benefit clients across multiple sectors.
Looking ahead, the manufacturer remains committed to advancing smart monitoring, predictive maintenance, and energy-efficient drive systems. Whether serving a clinical pharmacy, a high-volume drug producer, or an international distributor, the company provides the engineering depth and manufacturing integrity that define enduring excellence. For global partners, choosing this heritage brand means investing in reliability that spans generations of production.

 +8613809387113