For nearly three decades, one established manufacturer has been a cornerstone of industrial processing technology, earning the trust of pharmaceutical producers, hospital pharmacies, overseas distributors, and enterprises across the food, chemical, and agricultural sectors. As a director unit of the China Pharmaceutical Equipment Industry Association, the company has successfully delivered solutions to more than a thousand plants worldwide. Its enduring reputation is built on engineering depth, regulatory awareness, and a relentless commitment to smart, seamless production.
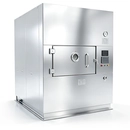
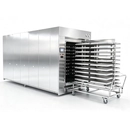
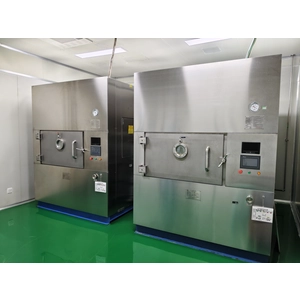
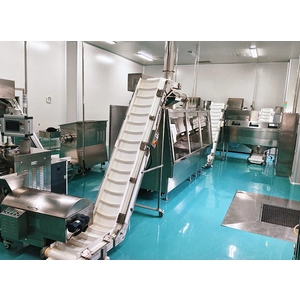
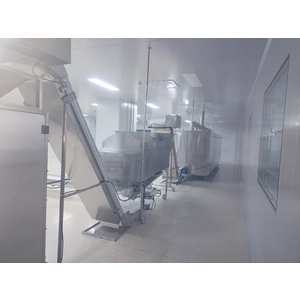
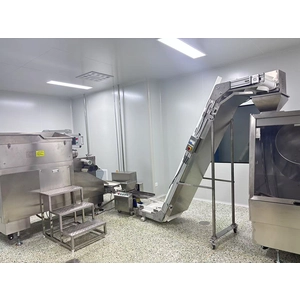
In continuous manufacturing environments, uninterrupted workflow and uniform heat distribution are paramount. The continuous conveyor drying machine china represents a significant leap forward, utilizing advanced airflow dynamics and multi-zone temperature controls to ensure even moisture reduction without halting the production line. This design minimizes manual handling and maximizes throughput, making it an indispensable asset for large-scale processors. The robust construction ensures reliable, long-term operation even under heavy continuous loads.
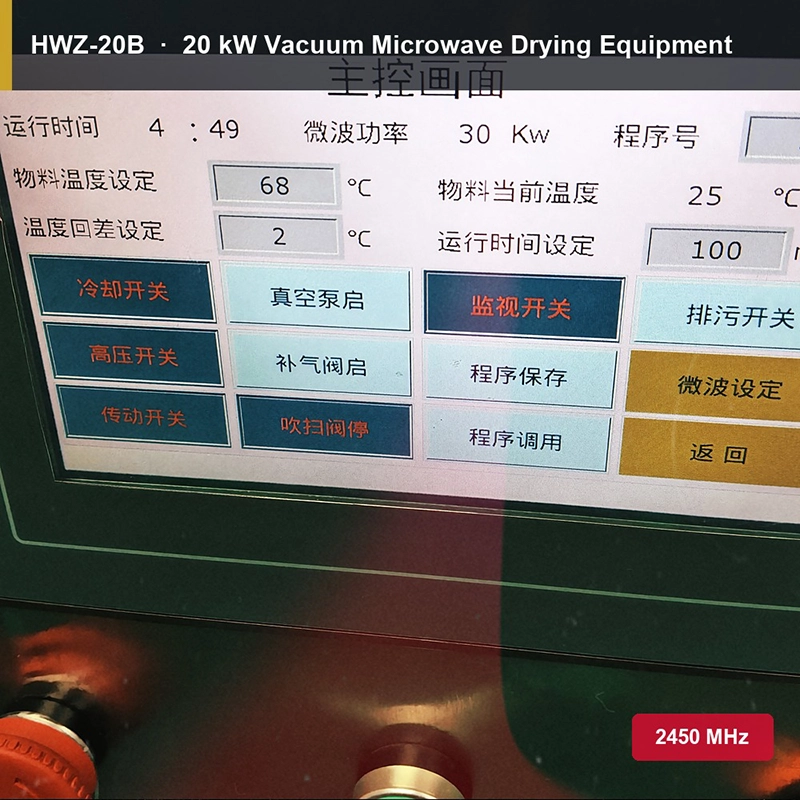
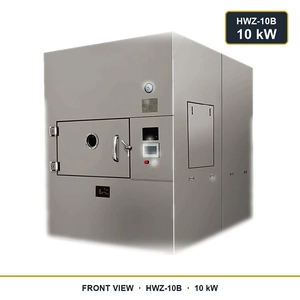
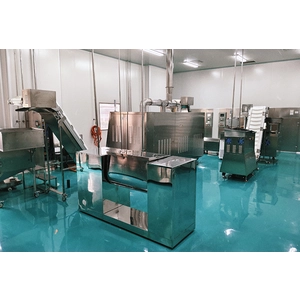
When it comes to sensitive active ingredients, precision is non-negotiable. As a highly respected pharmaceutical drying machine factory china, the company engineers systems that strictly adhere to GMP standards. These dryers incorporate gentle thermal profiles and precise humidity management to protect heat-sensitive botanical extracts and chemical compounds. By maintaining strict batch-to-batch consistency and providing comprehensive validation documentation, the equipment safeguards product integrity and simplifies regulatory compliance for drug manufacturers.
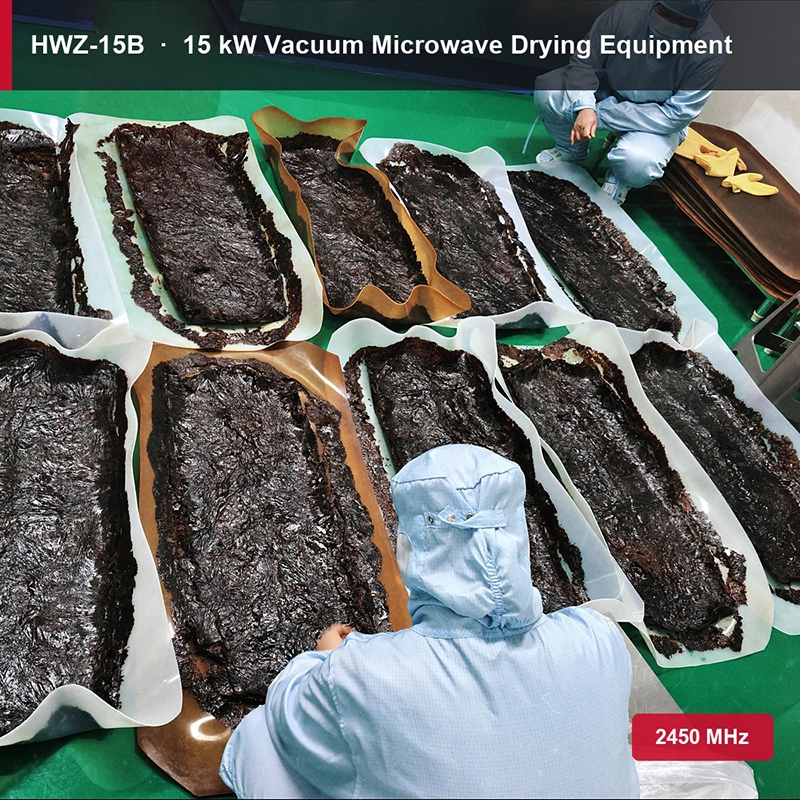
To meet the demanding requirements of modern, high-volume production, automation is essential. The automatic industrial drying line B2B platform integrates intelligent PLC controls, real-time monitoring, and energy-efficient drive systems into a cohesive, fully automated workflow. Designed for business-to-business scalability, these lines allow contract manufacturers and large enterprises to reduce labor costs and minimize downtime. With seamless integration into existing factory floors, the system delivers repeatable, high-quality output across multiple shifts.
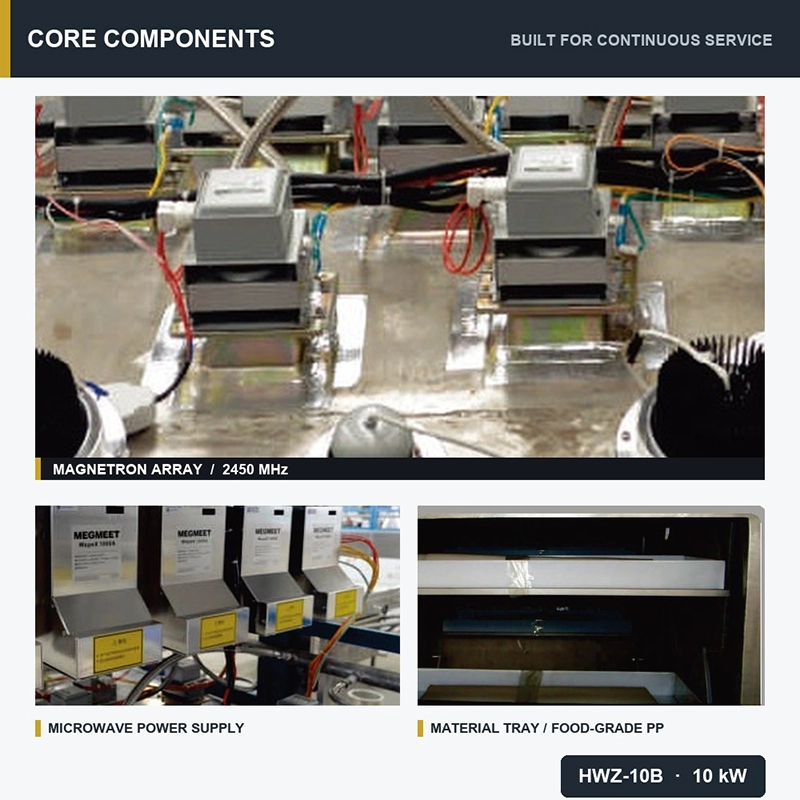
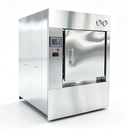
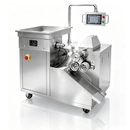
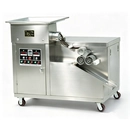
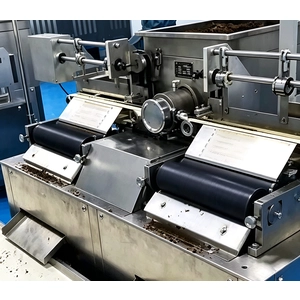
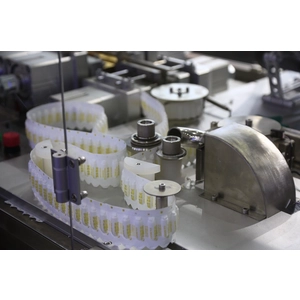
Beyond drying technology, the company’s comprehensive portfolio includes herbal pill making machines, fully automatic suppository filling and sealing lines, medical sterilization equipment, and chemical ball formers. Each product shares the same robust construction philosophy and intelligent control architecture. The extensive installed base and active role in shaping industry standards continue to drive refinements that benefit clients across multiple sectors, proving the company's versatility beyond a single application.
Looking ahead, the manufacturer remains committed to advancing smart monitoring, predictive maintenance, and sustainable energy practices across its entire range. Whether serving a clinical pharmacy, a high-volume drug producer, or an international distributor, the company provides the engineering depth and manufacturing integrity that define enduring excellence. For global partners, choosing this heritage brand means investing in a reliable foundation that spans generations of production.

 +8613809387113