In the competitive arena of pharmaceutical manufacturing, the ability to scale production efficiently while maintaining direct control over equipment sourcing can significantly impact operational success. For nearly three decades, one heritage manufacturer has empowered enterprises to achieve this balance, serving pharmaceutical companies, hospital pharmacies, overseas equipment dealers, and food and chemical processors with unwavering dedication. With a legacy of over one thousand successful installations and a vision of smart, seamless production, this industry leader continues to provide pill-making solutions that combine scalability, transparency, and proven performance.
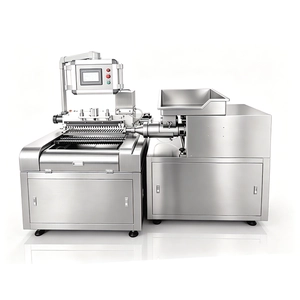
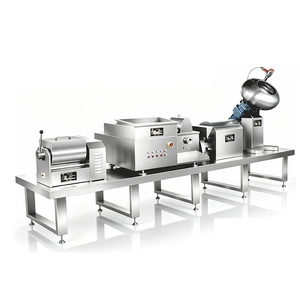
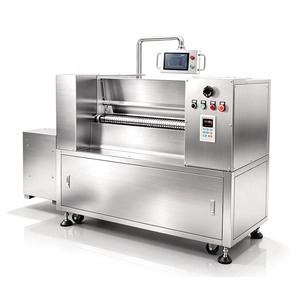
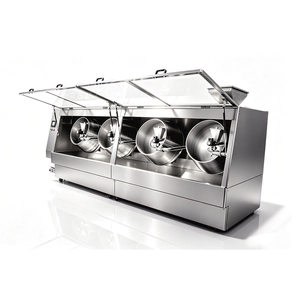
Major pharmaceutical groups and contract manufacturers often plan capacity expansions requiring multiple units, necessitating seamless coordination and harmonized specifications. The bulk order herbal pill making machine service is designed to accommodate volume commitments with flexible scheduling, synchronized delivery, and unified documentation for regulatory validation. Clients ordering fleets of machines benefit from interchangeable tooling, consistent control interfaces, and consolidated after-sales support, significantly reducing the complexity of multi-line integration. This systematic approach has made the company a preferred partner for global pharmaceutical chains establishing new production campuses or upgrading existing facilities with multiple identical units.
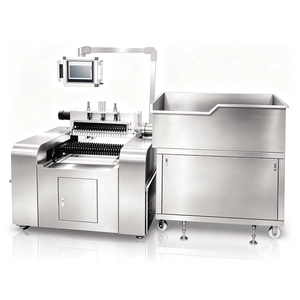
Perhaps the most compelling advantage lies in the direct relationship with the original equipment builder. The herbal pill making machine factory direct model eliminates unnecessary intermediaries, fostering transparent communication between end-users and the engineering team. This direct channel enables rapid customization, faster resolution of technical queries, and immediate access to design improvements and software updates. Moreover, factory-direct procurement ensures that every machine is accompanied by complete build records, factory acceptance test protocols, and training materials generated at the source – simplifying regulatory submissions and internal quality audits for pharmaceutical manufacturers worldwide.
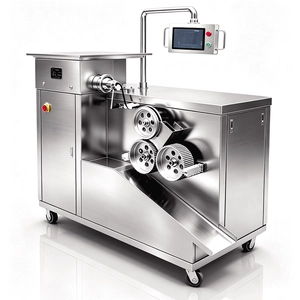
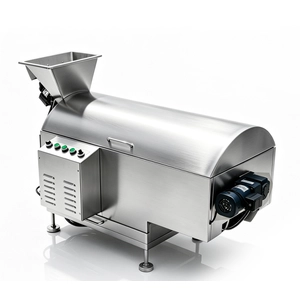
For enterprises seeking immediate deployment without compromising on quality, the availability of proven, ready-to-operate machinery is essential. The commercial herbal pill machine on sale represents a mature, field-tested platform that has been refined through decades of real-world production feedback. These machines are engineered to handle a wide spectrum of herbal formulations – from free-flowing granules to hygroscopic, heat-sensitive extracts – with precision compression and gentle forming techniques that preserve active ingredient integrity. The commercial availability of these units ensures that enterprises ranging from clinical compounding pharmacies to high-volume industrial facilities can access proven technology that delivers consistent pill weight, hardness, and dissolution characteristics from day one of operation.
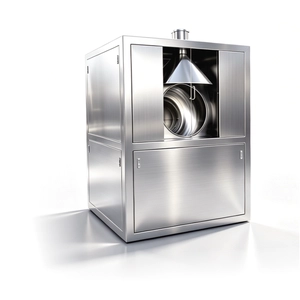
Complementing its pill-making expertise, Huayuan's comprehensive portfolio includes fully automatic suppository filling and sealing systems, continuous dryers, sterilization units, and chemical ball formers – all sharing the same robust construction and intelligent control architecture. As a director unit of the China Pharmaceutical Equipment Industry Association, the organization remains at the forefront of regulatory evolution and technological innovation, continuously incorporating field feedback into next-generation designs. This cross-sector proficiency, combined with a global installed base spanning over a thousand pharmaceutical plants, positions the company as a trusted partner for enterprises seeking reliable, adaptable, and commercially viable machinery that transcends conventional pill production.
Looking forward, this heritage manufacturer continues to invest in smart monitoring systems, predictive maintenance algorithms, and energy-efficient drive technologies, ensuring that every machine – whether procured through bulk orders, factory-direct channels, or commercial offerings – remains competitive throughout its operational lifecycle. Whether equipping a new production campus, upgrading existing lines, or establishing a global distribution network, clients benefit from the scalability, transparency, and proven performance that define this brand's legacy. For drug makers, dealers, and industrial processors across all scales, choosing Huayuan means partnering with a manufacturer that combines bulk-order capability, direct factory access, and commercially proven solutions – a combination that continues to drive success in the ever-evolving pharmaceutical landscape.

 +8613809387113